The commercial confectionery sector relies heavily on sophisticated industrial processes to meet growing global consumption. Operating a high-volume production facility involves managing numerous technical variables simultaneously. Successful retail distribution generally requires products that maintain strict structural and visual standards from the factory floor directly to the consumer store shelves.
Transitioning confectionery concepts from small-batch testing to massive commercial output presents notable engineering challenges. Large-scale cooking and depositing require highly calibrated machinery to prevent ingredient degradation. Modern manufacturing plants invest substantially in automated infrastructure to reduce manual handling and minimize the risk of human error during the most critical phases.
Balancing production speed with product integrity remains a primary objective for industrial operations. Rushing the cooking or setting phases frequently leads to compromised textures or shortened shelf life. Consequently, professional facilities prioritize steady, controlled manufacturing environments to support sustainable commercial growth and reliable output for their commercial partners.
How Gummy Candy Manufacturers Manage Batch Uniformity
Achieving consistent piece weights and uniform shapes across millions of units is a fundamental operational requirement. Irregularities in candy sizes can disrupt automated packaging lines and lead to inaccurate nutritional labeling. Maintaining precise dimensional control helps protect both brand equity and consumer trust in the overall brand.
Capable gummy candy manufacturers typically rely on advanced technological solutions to maintain this strict uniformity. Automated depositing systems represent a critical component of modern factory infrastructure. These machines distribute liquid candy mass into thousands of individual molds with remarkable speed and volumetric precision, minimizing costly material waste.
The initial cooking phase also demands rigorous oversight from skilled gummy candy manufacturers. Technicians must carefully monitor temperature levels to ensure gelling agents activate correctly without scorching delicate flavor compounds. Precise thermal management during this stage lays the foundation for a stable, high-quality finished confectionery product.
Formulating different recipes often requires adaptable machinery settings. For instance, processing plant-based pectin generally involves different handling temperatures compared to traditional gelatin bases. Capable gummy candy manufacturers maintain flexible equipment configurations to accommodate these diverse ingredient profiles while sustaining continuous high-volume production schedules.
The Curing Process and Moisture Control
After the depositing phase, the confections must undergo a controlled resting period known as curing. This vital step allows the liquid mass to solidify and achieve its final chewy texture. Rushing this stage can severely compromise the structural stability of the finished goods during their shelf life.
Proper curing takes place within specialized, climate-controlled drying rooms. Technicians carefully regulate ambient temperature and humidity levels to draw excess moisture out of the newly formed sweets. These strict environmental controls help prevent the candies from becoming overly sticky during subsequent packaging and handling procedures.
Managing moisture content is particularly important for products intended for long-distance maritime transport. Candies that retain too much water are generally more susceptible to melting or clumping when exposed to fluctuating external temperatures. A disciplined curing process significantly extends retail shelf life and preserves aesthetic appeal.
Once adequately dried, the pieces are separated from their starch molds. A professional gummies manufacturer will then apply a light coating of oil or wax to the surface. This protective barrier provides an appealing visual shine while further preventing individual pieces from sticking together inside the packaging.
Scaling Capabilities for a Global Gummies Manufacturer
Serving international retail markets requires robust capacity planning and adaptable production lines. Commercial buyers frequently rely on a dedicated gummies manufacturer to fulfill large wholesale orders on strict timelines. Facilities must maintain sufficient raw material reserves and operational bandwidth to prevent supply chain bottlenecks during peak seasons.
Production agility is equally important for navigating seasonal retail cycles. A versatile gummies manufacturer can efficiently transition between standard bulk orders and specialized holiday-themed items. This operational flexibility allows retail clients to capture impulse sales during peak consumer shopping periods without experiencing costly inventory stockouts.
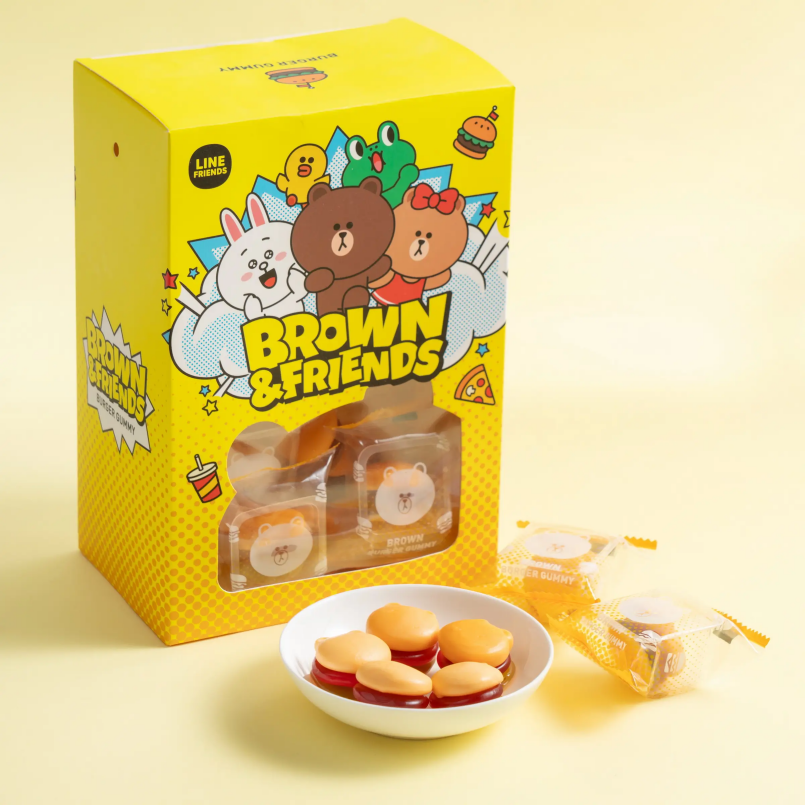
Advanced facilities also support the creation of intricate novelty designs, such as complex burger shapes or miniature cola bottles. Producing these detailed formats at scale requires sophisticated mold creation and highly accurate depositing equipment to ensure the visual details remain sharp and recognizable for the end consumer.
Advanced Manufacturing Infrastructure at HAPI
Organizations seeking reliable industrial partnerships frequently evaluate facilities based on their technical maturity. Operating as VIET NAM HONGRUN BIOLOGICAL FOOD CO., LTD, HAPI represents a modern production entity located in Bac Ninh, Vietnam. The organization leverages more than 25 years of established international confectionery manufacturing heritage.
To manage large-scale commercial output, HAPI utilizes automated NID starch mogul systems imported from Australia. This sophisticated machinery supports continuous, high-speed production while maintaining stringent quality control standards. Automated tray handling minimizes manual contact, supporting elevated hygiene levels across the entire manufacturing facility floor.
Beyond raw production capacity, HAPI employs five dedicated research and development experts. This technical team assists commercial partners in formulating stable recipes and designing custom shapes. Their ongoing support helps translate creative confectionery concepts into viable, shelf-ready products tailored specifically for global commercial retail distribution.
Maintaining strict safety certifications remains a core operational focus for HAPI. The facility implements rigorous daily sanitation protocols and comprehensive ingredient traceability systems. These disciplined quality assurance measures provide commercial buyers with confidence when sourcing high-volume product lines intended for international consumer markets and strict regulatory environments.
The Technical Backbone of Modern Candy Manufacturing
For commercial buyers, understanding a gummy manufacturer’s production capabilities is only one part of supplier evaluation. Buyers should also confirm batch specifications, agreed inspection criteria, sample approval procedures, packaging formats, and the availability of batch traceability records. Clarifying these requirements before production helps align manufacturing processes with product specifications, quality expectations, and distribution needs.